Food hygiene area solutions
Integrated Protection Solutions for Food Hygiene Areas
CleanroomLink helps food processing facilities maintain strict hygiene standards through integrated supply chain management. We provide the protective equipment, contamination control systems, and facility supplies necessary to meet international food safety regulations.
Consolidate procurement, reduce vendor complexity, and keep production environments compliant with solutions aligned to your HACCP, GMP, or ISO requirements.
The operational challenge
Hygiene control must work at production speed
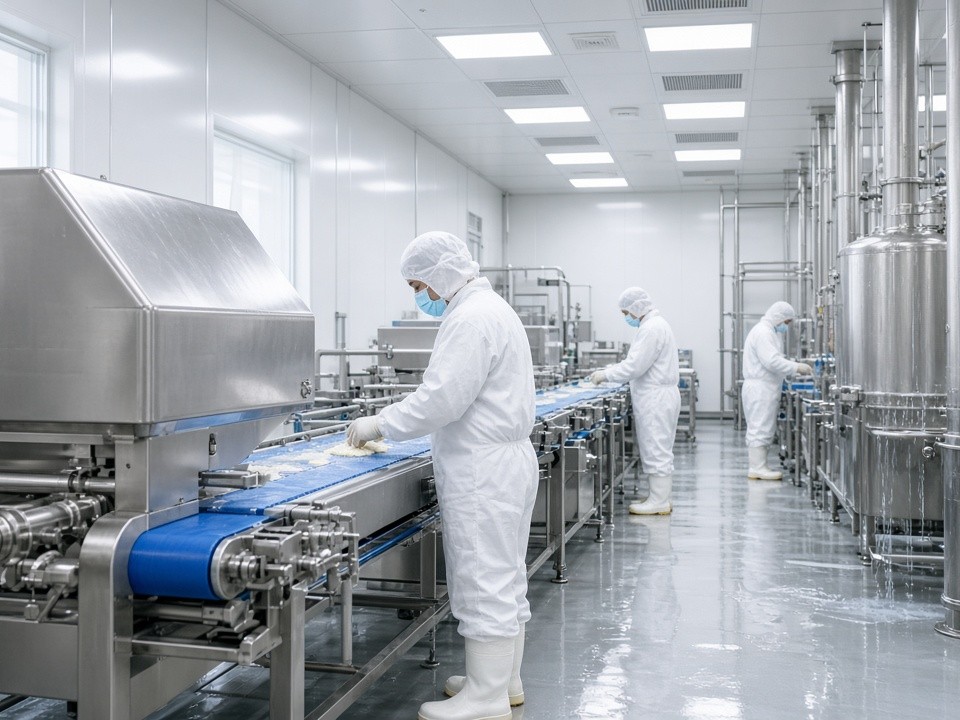
Food processing facilities face constant pressure to manage cross-contamination risks while maintaining production efficiency. Personnel hygiene, cleaning routines, slip prevention, and controlled movement between zones all need to work together.
Managing separate suppliers for PPE, cleaning consumables, and facility equipment can create fragmented procurement, inconsistent product quality, and compliance gaps.
CleanroomLink acts as a single integration partner. We align protective gear and facility equipment with your hygiene zoning, risk profile, and HACCP, GMP, or ISO requirements so every item serves a functional purpose in your contamination control strategy.
Zone-by-zone planning
Operational parameters for food processing zones
Effective contamination control requires different strategies for different areas. We help plant teams match personnel hygiene, cleaning, access control, and food-contact requirements to each zone.
| Area type | Hygiene risk | PPE | Gloves | Footwear | Cleaning supplies | Entry management | Food-contact requirements | Typical application |
|---|---|---|---|---|---|---|---|---|
| Raw material intake | Microbial contamination from incoming materials and traffic | Hairnets, beard covers, aprons | Blue nitrile gloves | Non-slip boots | Food-grade disinfectants | Sticky mats and boot scrubbers | Use food-safe materials where equipment or packaging may be contacted | Receiving docks, inspection points, and raw ingredient staging |
| High-care processing | Cross-contamination and pathogen transfer | Full coveralls, face masks, sleeves | Metal-detectable and cut-resistant gloves | Dedicated non-slip hygienic boots | Specialized cleaning and sanitation agents | Air showers and pass-through boxes | FDA- or EU-aligned materials and documented suitability for the application | Ready-to-eat processing, controlled production, and high-risk lines |
| Packaging and distribution | Particle contamination and handling-related transfer | Hairnets and protective gloves | Powder-free gloves | Clean, slip-resistant footwear | Dry cleaning supplies and surface wipes | Air filtration and gowning benches | Powder-free, low-shedding materials suitable for packaging environments | Finished product packing, dispatch, and distribution areas |
Integrated protection system
Three layers of contamination control
Personnel protection
Food-grade PPE including metal-detectable items, high-visibility garments, protective apparel, hair coverings, masks, sleeves, gloves, and aprons.
Designed for controlled hygiene routines
Work environment protection
Stainless steel worktables, protective mats, and surface covers that resist chemical cleaning agents and help prevent microbial growth.
Built around cleanability and slip prevention
Facility protection
Infrastructure for clean zones, including air shower systems, filtration units, and specialized pass-through boxes for controlled material transfer.
Supports separation between hygiene zones
Compliance-driven selection
Documentation and performance matched to your market
Compliance is non-negotiable in food production. We verify that supplied products align with the regulatory requirements and technical specifications of your target market.
Certification transparency
Receive test reports and certificates of conformity to support internal audits and external certifications.
Performance matching
Source EN-compliant PPE for European markets or FDA-compliant materials for North American operations.
Standardization
Create a consistent procurement list compatible with your facility procedures and hygiene protocols.
Supply chain strategy
A direct alternative to fragmented distribution
Plant managers need to balance cost, quality, and supply stability. Our sourcing model consolidates the categories that support day-to-day hygiene without compromising technical requirements.
Discuss your supply requirementsConsolidated procurement
Source consumables, PPE, and facility equipment through a single channel to reduce administrative overhead and shipping complexity.
Customized sourcing
Identify the right manufacturer for each use case, from certified products for high-risk zones to cost-optimized options for general production.
Stable supply
Maintain relationships with qualified manufacturers to support consistent availability and help prevent production interruptions.
How we support your facility
From risk review to ongoing supply support
-
Step 01
Requirements assessment
Review hygiene zones, risk factors, existing procedures, and procurement pain points.
-
Step 02
Solution design
Develop a customized product bundle that addresses contamination risks and budget requirements.
-
Step 03
Sourcing and quality control
Select products from qualified manufacturers and apply inspection standards before shipment.
-
Step 04
Ongoing support
Provide compliance documentation and product guidance as production requirements evolve.
Quality commitment
Accountability from specification to delivery
Every product provided by CleanroomLink is backed by a commitment to performance and transparency. If a product fails to meet the specifications agreed during sourcing, we address the issue directly in accordance with our commercial agreements. Our aim is to be a long-term partner, not just a vendor.
Request a consultation
Strengthen your food hygiene procurement plan
Whether you are upgrading an existing line or setting up a new production area, we provide the technical support and product sourcing needed to improve contamination control.
Contact details
CleanroomLink
Email:
Address:
Tell us about your facility
Share your hygiene zones, PPE requirements, cleaning needs, or target compliance standards and our team will help define the next step.